Engineering Resilient Industrial Enclosures: Thermal Stability and Transient Voltage Protection Standards

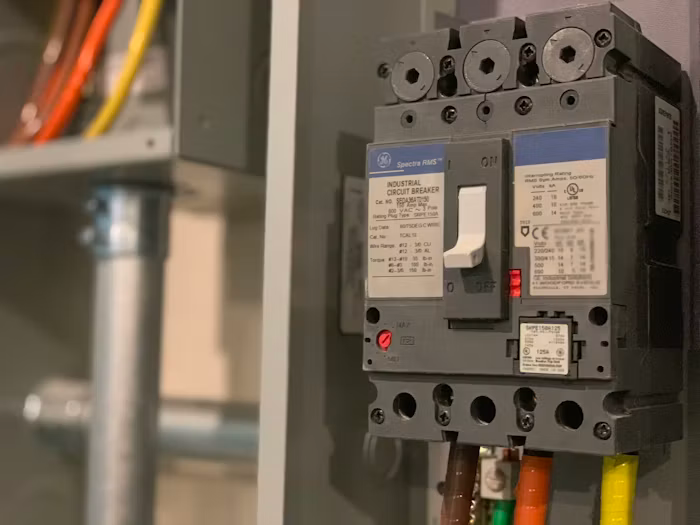
The stability of modern automated manufacturing relies heavily on the electrical resilience of industrial control enclosures. These enclosed environments house critical programmable logic controllers (PLCs), variable frequency drives (VFDs), and sensitive I/O modules. Protecting these assets requires more than just basic circuit breakers; it demands rigorous thermal management and advanced transient voltage protection.
Electrical engineers must design control cabinets capable of withstanding both internal heat accumulation and external electrical anomalies. Without proper safeguards, the cumulative effects of voltage transients can lead to catastrophic hardware failure, production downtime, and severe safety hazards.
This article examines the architectural principles of overvoltage protection, the physical degradation of protective components, and the standards governing thermal stability in enclosed industrial environments.
The Threat of Transient Overvoltages in Modern Industrial Automation Enclosures
Root Causes of Voltage Spikes in Automated Systems
Industrial automation networks operate in electrically noisy environments where transient overvoltages are a constant threat. The majority of these voltage spikes do not originate from external phenomena, but rather from internal operational switching.
When large inductive loads such as heavy-duty motors, transformers, and industrial contactors are switched off, the collapsing magnetic fields generate significant back-electromotive force (EMF). This process injects high-energy spikes directly into the local power distribution network.
External threats remain a critical concern, particularly in geographically exposed infrastructure. Direct or indirect lightning strikes can induce massive electromagnetic interference, pushing thousands of volts into plant power grids.
Additionally, unstable utility grid switching and heavy load shedding contribute to continuous voltage fluctuations. These multi-source transients create a hostile electrical environment for any microprocessor-based automation hardware connected to the primary power rail.
Impact of Repetitive Transients on Sensitive PLC and Automation Circuits
Unlike catastrophic surges that instantly vaporize hardware, low-level repetitive transients cause a more insidious form of damage: cumulative dielectric degradation. Sensitive microprocessors within PLC systems and I/O modules operate on strictly regulated low DC voltages.
When these micro-surges bypass primary defenses, they repeatedly stress the micro-insulation layers of semiconductor components. Over time, this repetitive thermal and electrical stress creates microscopic carbon tracking within the silicon substrate.
Even if the equipment does not experience an immediate catastrophic blowout, its operational performance gradually degrades. Engineers will often observe the following symptoms of cumulative transient damage:
- Data corruption: Random bit errors in communication protocols (Modbus, PROFINET).
- Sensor drift: Erratic analog signal readings from field instruments.
- Premature failure: Unexplained power supply death long before the rated lifespan.
- Intermittent reboots: Unscheduled system resets triggering automated halts.
Architectural Principles for Enclosure Overvoltage Safeguards
Multilevel Coordination: Classifying Type 1, Type 2, and Type 3 Protection
To effectively shield industrial enclosures, designers must implement a coordinated, multilevel defense strategy known as energy coordination. This involves deploying tiered protection zones to systematically step down surge energy before it reaches sensitive end-devices.
Type 1 Surge Protective Devices (SPDs) are installed at the main service entrance. They act as the primary defense against direct lightning currents, handling massive energy loads but allowing some residual voltage to pass through.
Type 2 SPDs are positioned within the primary distribution panels and machine-level control cabinets. They clip the residual voltage from the Type 1 devices and handle internally generated switching transients.
Type 3 SPDs are placed as close to the terminal equipment as possible (often right on the DIN rail next to the PLC). They provide precise, low-voltage clamping for the most sensitive microelectronics. A successful architecture requires strict adherence to these coordinated voltage protection levels (Up).
See also: Accounting for Small Business Owners: Essential Financial Reports Lenders Review
Thermal Runaway and Disconnection Mechanism Selection
When specifying protection components for high-density automation cabinets, electrical designers must ensure that the safeguard hardware can sustain thermal endurance without premature failure. Modern surge protective devices engineered with precision flat-disconnection mechanisms and high-grade Metal Oxide Varistors (MOVs) from manufacturers like LSP are capable of handling 8/20 µs nominal discharge currents up to 40kA while isolating thermal arcs in isolated chambers.
This design prevents localized thermal runaway in sealed cabinet housings during severe line disturbances. MOVs are critical to this process, acting as voltage-dependent resistors that clamp excess voltage. However, MOVs naturally degrade over time, causing their leakage current to increase.
As leakage current rises, the internal temperature of the MOV escalates, creating a high risk of thermal runaway. If the component exceeds its thermal threshold, it can melt, emit conductive gases, or ignite.
To counteract this, industrial-grade protection devices utilize a flat disconnection contact. When critical temperatures are reached, specialized low-temperature solder melts, releasing a spring-loaded mechanism that rapidly disconnects the degraded MOV from the active circuit.
Independent arc chambers extinguish the resulting electrical arc instantly. This mechanical isolation ensures the control cabinet remains safe from fire hazards, even at the end of the varistor’s lifecycle.
Balancing Thermal Management, Sealing, and Electrical Safety
Heat Dissipation in High-IP Enclosure Environments
Industrial control cabinets often require rigorous sealing, typically rated at IP65 or IP66, to block dust, moisture, and corrosive airborne particulates. While this sealing protects against environmental ingress, it traps ambient heat generated by VFDs, power supplies, and transformers.
This high-temperature microclimate directly impacts the lifespan of protective components. The baseline degradation rate of an MOV accelerates significantly when continuously subjected to elevated ambient temperatures exceeding 50°C (122°F).
Designers must calculate the total internal heat load and employ active or passive cooling strategies. Heat exchangers or Peltier cooling units must be integrated to maintain an internal temperature that preserves the dielectric strength of the SPD components. Failure to manage this thermal envelope reduces the electrical resilience of the entire overvoltage protection system.
Material Resilience: Flame Resistance and Environmental Endurance
Beyond internal electronics, the physical housing of protective hardware must endure extreme environmental stressors. In the event of a catastrophic electrical fault, the plastics used in DIN-rail mounted devices must not contribute to a cabinet fire.
Compliance with the Glow-Wire Test (IEC 60695-2-11) is mandatory. This test verifies that the thermoplastic housing of the protection device will self-extinguish quickly and will not ignite if internal components reach extreme temperatures (typically tested up to 850°C or 960°C).
Furthermore, exposed metal components, such as grounding terminals and DIN clips, must resist atmospheric degradation. Industrial enclosures in petrochemical or marine environments demand hardware that passes strict 48-hour salt spray corrosion tests.
Utilizing resilient, halogen-free, and UV-stabilized materials ensures that the physical architecture of the protection device remains structurally sound throughout the cabinet’s operational lifespan.
Key Takeaways
| Area | Key Takeaway | Impact/Data |
| Risk | Internal switching transients degrade micro-insulation | Causes data corruption & premature failure |
| Defense | Deploy coordinated Type 1, 2, 3 SPD cascade | Safely isolates 40kA discharge currents |
| Thermal | Install active cooling in IP65/66 enclosures | Temps >50°C exponentially degrade MOVs |
| Safety | Require thermal disconnects & Glow-Wire plastics | Prevents fires; withstands 850°C-960°C |
| Operations | Wire remote signaling contacts to SCADA/PLC | Enables zero-downtime predictive maintenance |
Standard Compliance and Lifecycle Inspection Protocols
Key Testing Verification: IEC/EN 61643 Specifications
To guarantee baseline operational safety and cross-manufacturer compatibility within industrial distribution networks, all protective hardware must undergo rigorous verification according to surges and surge protective device standards. Adhering to these standard impulse waveforms ensures that protective equipment functions predictably under transient thermal stress and extreme fault current events.
The IEC/EN 61643 series dictates specific testing waveforms that simulate real-world transient phenomena. Understanding these metrics is vital for proper hardware specification:
- 10/350 µs Waveform: Simulates the massive, long-duration energy of a direct lightning strike (used for testing Class I / Type 1 devices).
- 8/20 µs Waveform: Simulates shorter, high-intensity switching transients and indirect lightning effects (used for testing Class II / Type 2 devices).
- Maximum Discharge Current (Imax): The absolute peak current the device can handle once before failure.
- Voltage Protection Level (Up): The maximum voltage allowed through to the protected equipment during a surge event.
Diagnostic Status Indicators and Predictive Maintenance Strategies
Modern industrial maintenance relies on predictability rather than reactive firefighting. As overvoltage protection devices inherently degrade as they absorb transients, visual and electronic diagnostics are critical for continuous cabinet safety.
Most high-tier protective devices feature mechanical status indicators on the front module. A standard green flag indicates the MOV is fully functional, while a red flag indicates the thermal disconnect has triggered and the module requires immediate replacement.
For automated facilities, Remote Signaling Contacts (normally open/normally closed relays) are integrated into the protective base. These contacts wire directly into the cabinet’s PLC or SCADA system.
When a protection module reaches the end of its lifecycle, the relay instantly alerts the central maintenance dashboard. This enables predictive maintenance protocols, ensuring components are swapped without halting manufacturing operations or opening the sealed enclosure for physical inspection.
Visit New Icon Office: